Quality assurance frameworks rely heavily on independent physical product evaluations across manufacturing facilities. Integrating external inspection services helps organizations maintain strict compliance standards across complex global production networks. Systematic evaluation protocols verify that finished goods match detailed engineering specifications prior to market distribution.
Standardized quality checks identify operational defects before products reach commercial supply chains. Independent testing protocols confirm structural integrity, material safety, and functional accuracy during production runs. Consistent monitoring protects consumers while reducing financial losses associated with product recalls.
Defining Quality Assurance in Modern Manufacturing
Quality assurance focuses on preventing defects through systematic production monitoring and operational testing. Standardized evaluation protocols verify that factory operations align with specified engineering guidelines continuously. Prevention measures reduce material waste while maintaining uniform product characteristics across high-volume assembly lines.
Factory managers rely on objective data to identify process variations during manufacturing operations. Regular physical checks track component dimensions, material density, and assembly accuracy against technical blueprints. Data collection helps technicians adjust machinery before non-conforming parts move down assembly lines.
Systematic quality frameworks integrate raw material testing, in-line reviews, and final product audits. Multi-stage testing ensures that defective components are removed before final packaging occurs. Comprehensive quality systems maintain consistent product output across diverse manufacturing environments.
Regulatory Compliance and Safety Verification
Legal frameworks require strict adherence to international safety, electrical, and environmental protection regulations. Independent reviews verify that finished goods meet local market safety laws before distribution begins. Regulatory compliance prevents product seizures, financial penalties, and legal disputes at border crossings.
Certifying agencies conduct specialized laboratory testing to screen for hazardous chemicals and heavy metals. Testing protocols verify that consumer goods meet health standards established by government agencies. Compliance documents provide verified proof of product safety for international trade authorities.
Documented test results accompany international freight shipments during customs clearance procedures. Clear compliance records speed up import processing times and prevent cargo holds at ports. Verified regulatory alignment ensures smooth cross-border trade operations for commercial importers.
Raw Material Audits and Supply Chain Security
Quality assurance begins with raw material verification before factory assembly processes commence. Inspectors evaluate incoming sub-components to verify compliance with contractual material specifications. Early testing prevents substandard raw materials from entering primary production streams.
Sub-tier supplier evaluations track raw material origin, chemical composition, and physical strength metrics. Material certifications confirm that raw inputs meet structural requirements before factory workers process them. Component checks prevent early structural failures in final assembled products.
Verifying supplier consistency builds reliable supply chain networks across international manufacturing hubs. Consistent raw material quality reduces factory downtime and keeps production schedules running smoothly. Material oversight maintains baseline product quality before mass manufacturing begins.
In-Process Monitoring and Operational Control
Mid-production testing monitors assembly line accuracy while factory workers execute active orders. Technicians examine random product samples taken directly from operational assembly lines. In-line reviews identify machinery wear and operational errors before full order completion.
Identified assembly flaws trigger immediate mechanical adjustments on active factory floors. Machinery recalibration stops the continuous production of defective physical units during long runs. Early operational intervention saves expensive raw materials and maintains target delivery dates.
In-process checks verify that factory workers follow standardized assembly steps consistently across shifts. Workmanship evaluations ensure proper mechanical joining, electrical wiring, and surface finishing. Continuous oversight maintains high manufacturing standards throughout extended production operations.
Final Product Verification and Acceptance Sampling
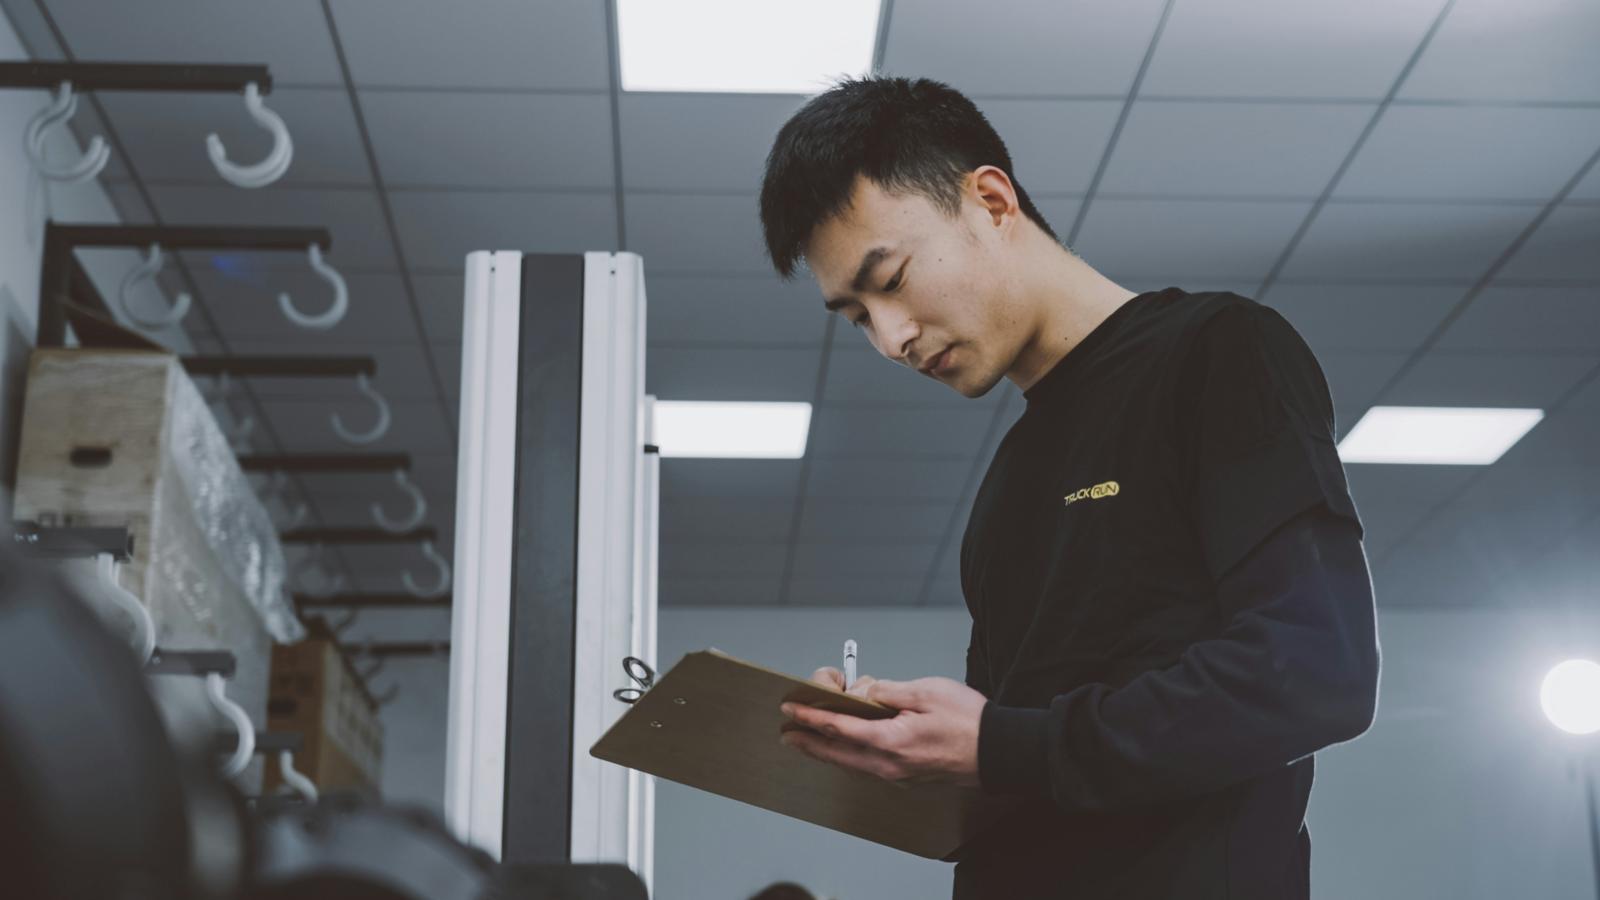
Pre-shipment testing takes place after factory workers complete assembly and packaging tasks. Inspectors select random product units using established statistical sampling tables for testing. Sample sizes reflect total order volumes to ensure statistical accuracy during physical checks.
Engineers test product operation, packaging durability, labeling accuracy, and physical shipping dimensions. Barcode verification ensures that outer shipping boxes match international logistics tracking data. Thorough checks confirm that finished shipments meet all buyer technical requirements.
Acceptable quality limits determine whether production batches meet contractual release standards. Passing inspection results allow factory managers to release goods for shipping container loading. Final verification ensures that buyers receive fully functional products that meet expectations.
Risk Mitigation through Independent Audits
Third-party testing provides objective evaluations unbiased by factory output pressures or delivery timelines. External auditors report physical findings directly to buyers without conflict of interest. Independent oversight provides accurate data regarding actual factory production quality levels.
Unbiased reporting helps management identify systemic supply chain risks across regional supplier bases. Risk assessments highlight specific manufacturing steps that produce high defect rates over time. Targeted corrective actions fix underlying operational issues before major product failures occur.
Independent documentation strengthens legal contracts between international buyers and overseas manufacturing plants. Clear inspection reports resolve commercial disputes regarding product quality and specification deviations. Objective data supports fair commercial decisions across complex global trade networks.
Key Takeaway
Maintaining product standards requires consistent operational oversight across global manufacturing networks. Implementing independent inspection services safeguards product quality effectively while ensuring continuous regulatory compliance. Systematic quality verification protects brand reputation, lowers operational risks, and guarantees product reliability.


Share this page with your family and friends.